Cap Inspection For Tetra Pak Bags that keeps fast lines audit ready
On high-speed Diamond Packaging lines, small cap and inkjet issues can quickly turn into rework, customer complaints, or traceability gaps. Cap Inspection For Tetra Pak Bags is positioned to stop those problems at the line—by inspecting cap quality and inkjet printing quality online, then rejecting unqualified packs before they move further.

Where Cap Inspection For Tetra Pak Bags fits on the line
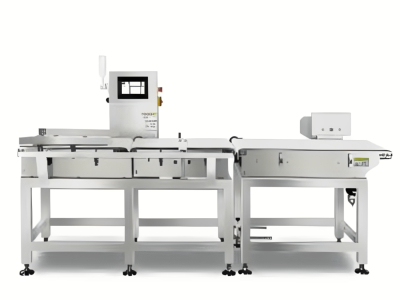
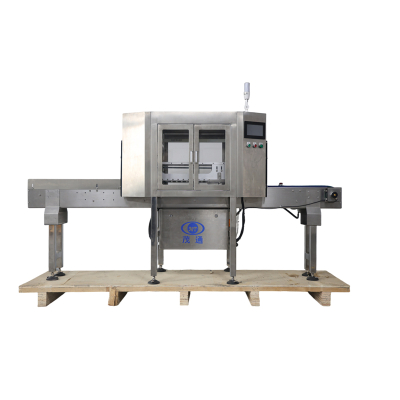
The Cap Inspection For Tetra Pak Bags system is designed for on-site installation 1.5–2 meters straight behind the capping machine. This placement supports real-time verification while packs are still in a controlled, repeatable position—an important condition for stable inspection and consistent rejection behavior.
For buyers evaluating Cap Inspection For Tetra Pak Bags, the most practical starting point is confirming a straight run of conveyor space in that location and clarifying which cap and inkjet failure modes must be intercepted online.
How Cap Inspection For Tetra Pak Bags works in six steps
In operation, Cap Inspection For Tetra Pak Bags uses a non-contact approach intended to avoid physical impact or damage to products.
The detection flow is commonly understood as a closed loop from sensing to rejection:
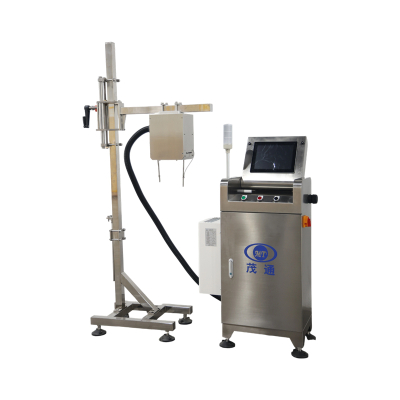
Because Cap Inspection For Tetra Pak Bags is built around inline imaging and digital analysis, it can support continuous quality checks at production speed—while keeping inspection and rejection decisions visible to operators through the HMI.
What 360° inspection targets in practice
A key expectation for Cap Inspection For Tetra Pak Bags is coverage: the system is designed for comprehensive 360° cap inspection and 360° inkjet code inspection. In production terms, this means it focuses on common, high-impact defects that can escape manual sampling.
The product description also emphasizes zero-delay cap inspection, designed to be unaffected by cap material, color variation, or packaging material interference.

Detection accuracy and what the numbers mean for procurement
For many procurement teams, acceptance criteria for Cap Inspection For Tetra Pak Bags come down to two things: rejection rate (catching true defects) and false detection rate (avoiding unnecessary waste and line disruption).
The following inspection accuracy table is presented as standard performance values.
| Inspection Items | Inspection Contents | Rejection Rate | False Detection Rate |
|---|---|---|---|
| Bottle Cap Inspection | Absent cap | ≥99.99% | <= 0.01% |
| Bottle Cap Inspection | Cap misalignment (offset from center: 5mm max) | ≥99.99% | <= 0.01% |
| Bottle Cap Inspection | Cap rotation (vertical distance difference between top/bottom ≥ 5mm) | ≥99.99% | <= 0.03% |
| Inkjet Printing Inspection | No inkjet print | ≥99.99% | <= 0.01% |
| Inkjet Printing Inspection | Overall inkjet print missing > 50% | ≥99.99% | <= 0.01% |
| Inkjet Printing Inspection | Overall inkjet print missing > 30% | ≥99.96% | <= 0.01% |
| Inkjet Printing Inspection | Deformed (stretched, squeezed), duplicated, or reversed packaging print | ≥99.98% | <= 0.01% |
In commercial practice, buyers typically align these targets with their product and packaging situation and confirm final acceptance criteria in the contract agreement.
Reliability features buyers ask for on fast lines
Industrial-grade cooling and IP65 protection
For long running shifts—especially in hot seasons—line stability often depends on thermal management and enclosure protection. Cap Inspection For Tetra Pak Bags is described with an industrial-grade cooling system intended to ensure stable operation and prevent faults during extended summer use, along with an IP65 safety protection rating.
Smart rejection control with optional line stop logic
Beyond simply ejecting defects, Cap Inspection For Tetra Pak Bags includes smart rejection control. In addition to automatic online rejection of defective caps or inkjet printing, the system supports automatic line stop after a preset number of consecutive defective rejections—a setting many plants use to surface recurring upstream problems faster.
Defect image traceability and operator access control
For audits and root-cause reviews, Cap Inspection For Tetra Pak Bags supports defect traceability by automatically storing images of defective caps. The storage period can be customized. The HMI provides multi-level access control, helping teams separate daily operation from parameter changes.
Remote monitoring and equipment control
For multi-site teams or limited on-shift engineering coverage, Cap Inspection For Tetra Pak Bags also offers 24/7 remote monitoring and equipment control service, which can support operation and management without waiting for on-site response.
Core configuration points to confirm before line integration
When specifying Cap Inspection For Tetra Pak Bags, procurement and engineering teams typically confirm the following items early:
For wider carton-line checks beyond caps and codes, buyers may also review the related category page for a broader Tetra Pak Inspection Machine selection.
Getting product details and configuration
For detailed specifications and configuration discussion, the product page for Cap Inspection For Tetra Pak Bags is the primary reference.
For direct contact, use WhatsApp.