Health Product Bottles Infrared Imaging Inspection Keeps Seals On Track
In high-throughput packaging, aluminum foil seals are often verified too late—after downstream handling has already added cost and complexity. Health Product Bottles Infrared Imaging Inspection closes that gap by integrating seal-quality verification directly inline, immediately after electromagnetic (induction) sealing. Using non-contact infrared thermal imaging, it evaluates the heat distribution pattern on each cap surface, flags abnormal patterns that indicate sealing defects, and links results to downstream rejection through adaptive tracking.

Why Inline Seal Inspection Matters at 300 Bottles Per Minute
With PET/PE bottles that use aluminum foil seals, the seal is created by electromagnetic heating that melts the heat-sealing film. The moment after sealing is also when thermal evidence of the process is most visible. The Health Product Bottles Infrared Imaging Inspection system is designed to use that brief window effectively—capturing the cap-surface heat distribution from the sealing step and transforming it into an inspection decision without making contact with the product.
This system functions as a fully automated inspection solution for aluminum foil seal quality on PET/PE bottle caps, achieving a maximum throughput of over 300 bottles per minute and featuring adaptive product tracking to support high-speed line operation.
How Infrared Thermal Imaging Indicates Seal Quality
The inspection method relies on sealing physics:
This captured heat distribution directly reflects the degree of compression between the gasket and the bottle cap, which indirectly reflects the seal quality. When a seal defect occurs, the heat distribution becomes abnormal.

For production teams, the relationships between common process causes and thermal indications can be summarized:
| Cause of defect | Defect type | Heat distribution indication |
|---|---|---|
| Aluminum film problems | Missing, damaged, inverted | Incomplete heat distribution |
| Capping machine problems | Loose cover, crooked cover | Insufficient heat conduction, low temperature |
| Electromagnetic sealing problems | False seal, over-seal | Temperature too high or too low |
Ultimately, this makes the Health Product Bottles Infrared Imaging Inspection system a non-contact, inline inspection step, intrinsically tied to the preceding sealing process.
Processing, Tracking, and Rejection in One Sequence
Speedy inspection only delivers value when it remains synchronized with the product flow. This system combines thermal image capture with software analysis and line integration features for stable operation at high speeds.
The Health Product Bottles Infrared Imaging Inspection system boasts several key capabilities, such as:
Performance and Application Range
| Item | Specification |
|---|---|
| Maximum inspection speed | Over 300 bottles/minute |
| Detection rate | ≥99.99% |
| False rejection rate | ≤0.03% |
| Applicable cap diameter | 20–200 mm |
| Applicable bottle diameter | 25–250 mm |
| Bottle height | ≤500 mm |
Installation Location and Site Requirements
As the inspection hinges on the thermal pattern from induction sealing, its precise placement on the conveyor is fundamental, not merely optional.
The installation location is specified as downstream of the electromagnetic sealer on a 1.5–2 m straight conveyor section.
Site preparation requirements include:
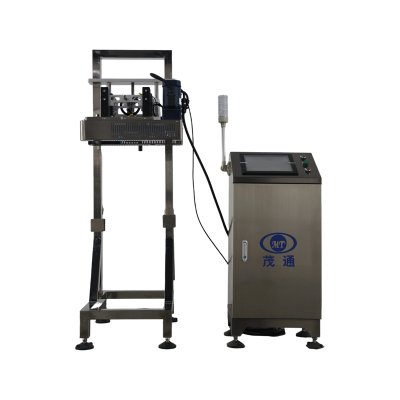
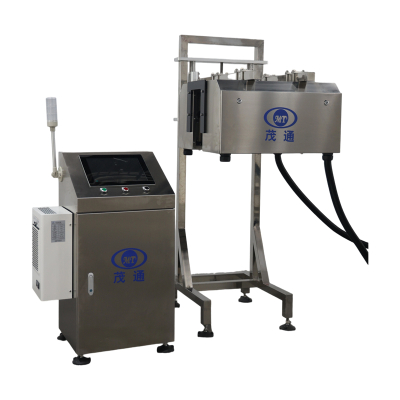
Equipment Structure
Operating Safety for Real Production Environments
Safety protocols are most effective when integrated into both commissioning and routine operations. The operating precautions for Health Product Bottles Infrared Imaging Inspection emphasize trained personnel, keeping protective covers in place, and avoiding unsafe interaction with rejection mechanisms and sensors.
Core Safety Requirements
Confirmations Prior to Commissioning
Before integration, confirm that bottle and cap sizes fall within the stated ranges, that the line can provide the specified straight conveyor section after the electromagnetic sealer, and that power, grounding, and compressed air meet the stated requirements. To learn more about product specifics and configuration options, please visit the official page for Health Product Bottles Infrared Imaging Inspection.