Configure a PE Bottle Squeeze Leak Detection Machine for 0.02 MPa
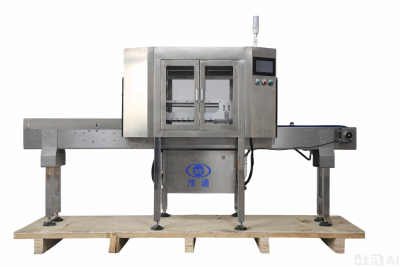
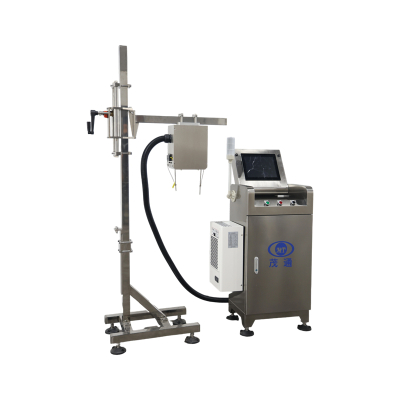
Accurate inline leak control is one of the fastest ways to stabilize packaging quality, reduce customer complaints, and limit unplanned downtime. The PE Bottle Squeeze Leak Detection Machine is designed for online pressure inspection of gas- or steam-containing PE/PET bottles, using belt squeeze detection and dual-sensor comparison to identify leaks and remove nonconforming products automatically.
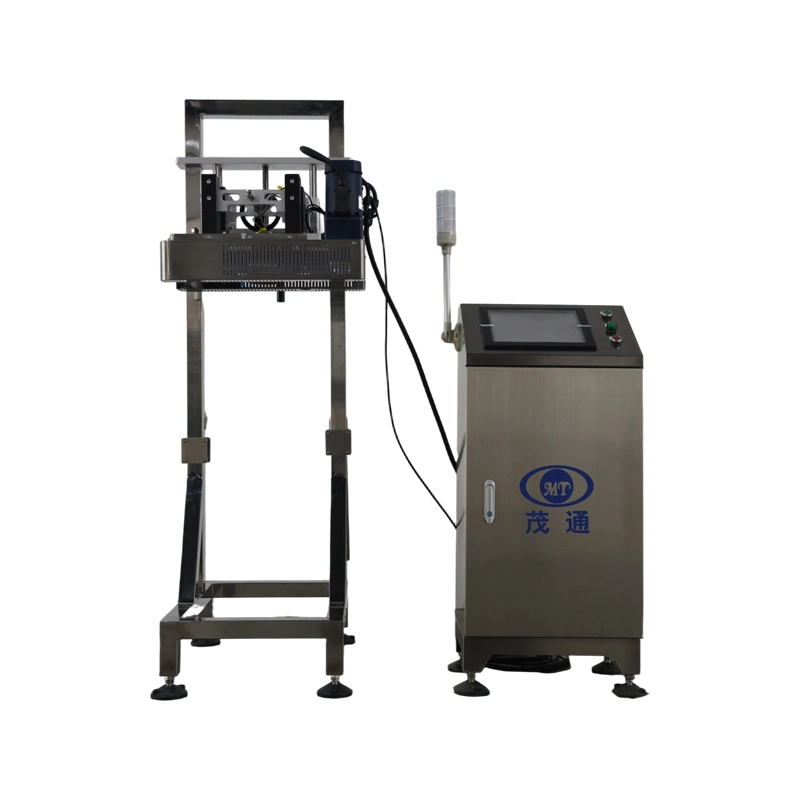
How the PE Bottle Squeeze Leak Detection Machine checks bottles in motion
On high-speed lines, a leak test only adds value when it stays synchronized with conveyor flow and still produces stable measurements. In the PE Bottle Squeeze Leak Detection Machine, bottles move through a controlled squeeze zone created by a flexible belt. A guide mechanism at the inlet pre-squeezes the bottle to maintain a certain pressure. If a bottle leaks, pressure is released as fully as possible during the squeeze period.
The decision logic is based on two pressure readings:

The platform includes adaptive speed tracking and stops automatically when the production line stops. It also lists an impact light alarm function, a Chinese language menu, Maotong’s unique DSP digital signal processing algorithm, a 24-hour remote assistance function, and a continuous rejection shutdown function.
Detection accuracy and performance parameters to verify on your line
For buyers comparing inline solutions, the core question is whether the PE Bottle Squeeze Leak Detection Machine can hold its specified targets under real conveyor conditions. The following parameters are stated for the equipment:
| Parameter | Specification |
|---|---|
| Detection range | 0.08 to 0.5 MPa |
| Accuracy | Better than 0.02 MPa |
| Rejection rate | ≥99.99% |
| False reject rate | ≤0.03% |
| Maximum inspection speed | Exceeds 600 bottles/minute |
A second table defines leak-test outcomes under specific conditions:
| Test item | Testing conditions and accuracy | Rejection rate | False kick rate |
|---|---|---|---|
| Air leakage detection | Visible air leakage at the aluminum film, low filling capacity, or pore size >0.8 mm | >99.99% | ≤0.03% |
| No cover detection | — | >99.999% | — |
To keep expectations realistic, it helps to evaluate each metric separately. Accuracy (pressure measurement capability) is not the same as rejection rate (how consistently defects are removed) or false reject rate (how often acceptable bottles are kicked). A well-set PE Bottle Squeeze Leak Detection Machine is typically assessed against all three during commissioning.
What can influence the 0.02 MPa target in daily production
The PE Bottle Squeeze Leak Detection Machine states accuracy better than 0.02 MPa, with practical notes about what can disturb measurements or cause false rejections.
Excessive vertical vibration of the conveyor chain will affect detection accuracy.
Beyond conveyor vibration, two additional factors are called out as influencing inspection results:
Operationally, the stated recommendation is to inspect products after cooling—ideally on a single-row conveyor belt exiting the sterilizer or where product temperature is uniform. In other words, to protect the performance of a PE Bottle Squeeze Leak Detection Machine, the most valuable “configuration” work often happens in the conveyor and process conditions around the machine.
Installation conditions that help keep rejection stable
A PE Bottle Squeeze Leak Detection Machine is intended for inline installation, and its installation guidance focuses on alignment, utilities, and a straight conveyor section for stable transport.
| Item | Recommended condition |
|---|---|
| Installation position | Install the equipment horizontally |
| Belt alignment | Clamping conveyor belt parallel to the product conveyor belt |
| Straight conveyor section | 1.5–2 meters |
| Power supply | Single-phase AC 220V, 50Hz |
| Total power | 250W |
| Compressed air | 4–8 bar |
| Ambient temperature | 0°C–50°C |
| Relative humidity | 10%–80% |
Before powering on, installation notes emphasize checking cables for looseness and confirming the grounding wire of the control box.
If your goal is to preserve the specified rejection rate and false reject rate, a simple commissioning habit is to verify alignment (horizontal mounting and parallel belts) and then observe whether any vertical conveyor vibration appears during normal speed changes. These checks directly support more consistent readings in the PE Bottle Squeeze Leak Detection Machine.
When buyers shortlist this machine alongside pressure inspection equipment
Many packaging teams build a family of inspections around pressure integrity. For example, the Can Pressure Tester is described as a fully automated pressure inspection system with adaptive speed tracking and a listed testing capacity over 1,200 cans per minute.
When comparing options, buyers typically map container type and speed requirements first, then confirm whether a PE Bottle Squeeze Leak Detection Machine fits the available 1.5–2 m straight conveyor section and whether utilities match (220V single-phase power and 4–8 bar compressed air).
For product details, see the official listing for the PE Bottle Squeeze Leak Detection Machine, and for pressure inspection in the same category, the Can Pressure Tester.
If you need installation or application confirmation, the official contact information provided is: +8618612569280 and qibin@maotongtech.com.