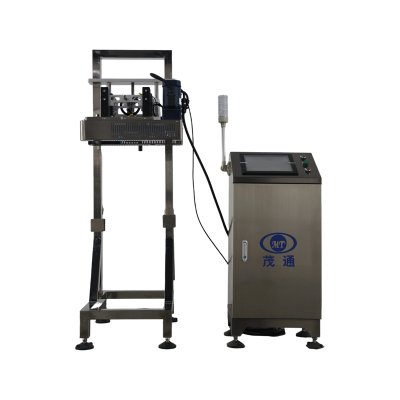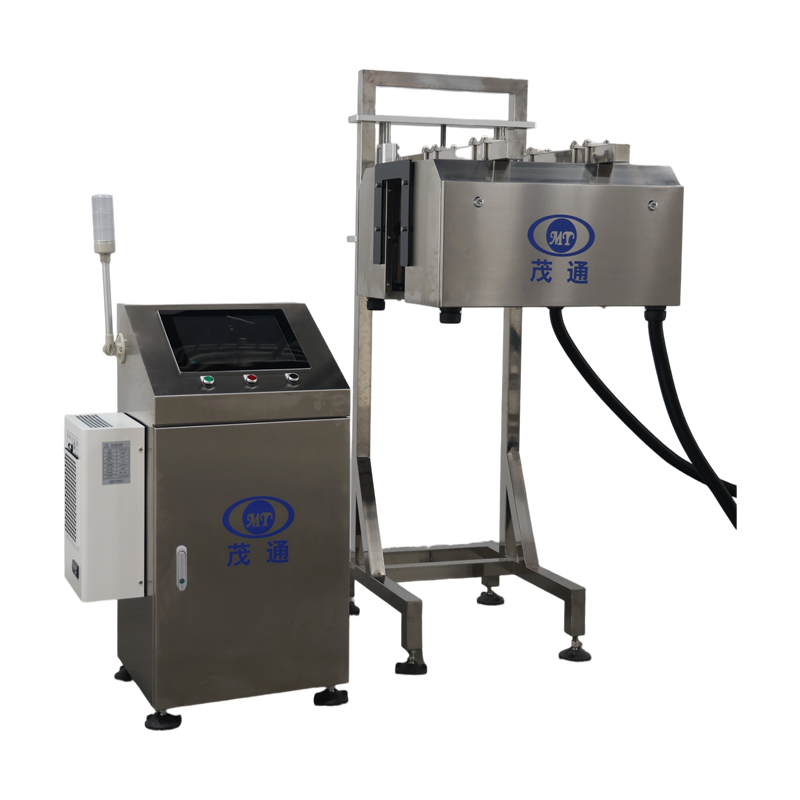
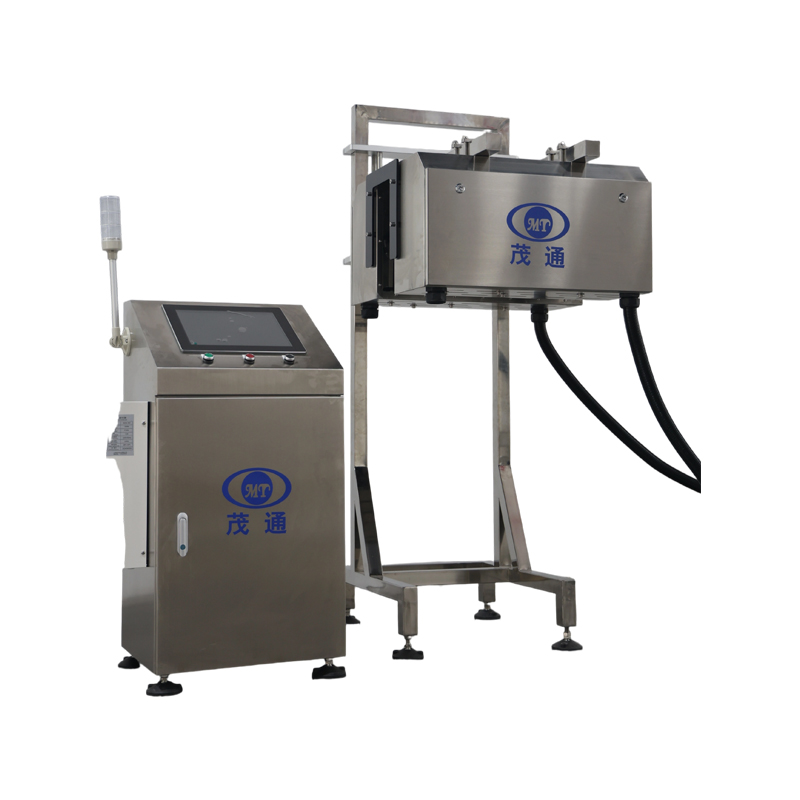
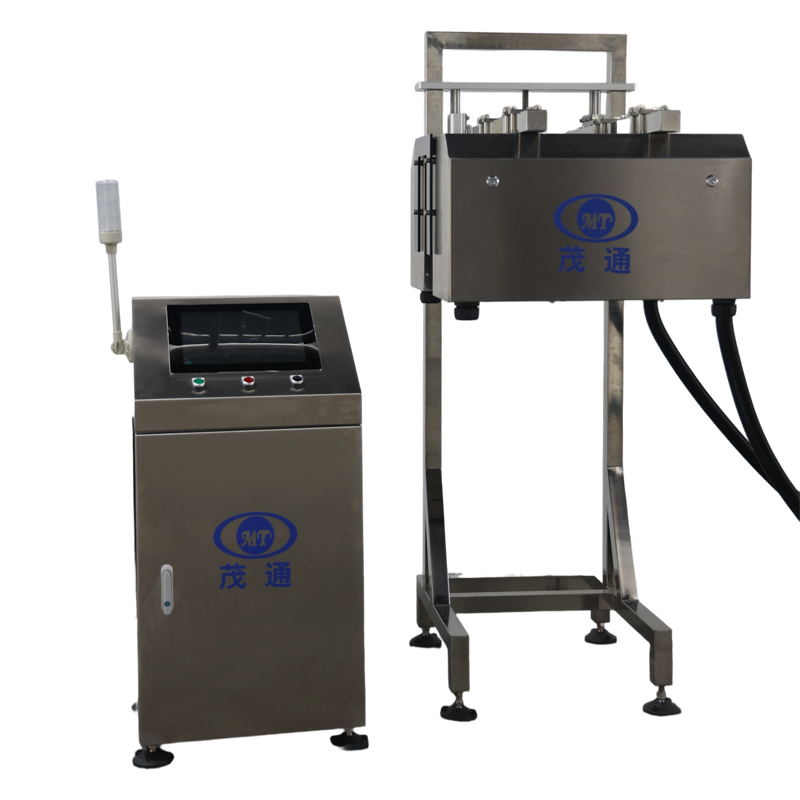
PET Label Inspection Machine
1.360 degree inspection
2.Muli view stiching and color recogniton technology are more reliable
3.The maximum speed is up to 36000 BPH
I. Project Design Basis
1. Project Overview
1.1 Project Name
PET Bottle Label Online Inspection System
1.2 Project Scope
The proposed system utilizes advanced machine vision technology to perform fully automated, non-contact online inspection of PET bottle labels. The inspection functions include label presence detection and label height verification to ensure that labels meet the specified production requirements.
1.3 Designed Production Capacity
60,000 bottles per hour
1.4 Applicable Containers
PET bottles
2. Environmental Requirements
2.1 Installation Altitude
The equipment is designed for operation at altitudes ranging from 5 to 3,000 meters above sea level.
2.2 Recommended Operating Temperature
5°C to 40°C
2.3 Recommended Relative Humidity
50% to 65% RH
2.4 Factory Site Requirements
The installation area shall comply with applicable national standards and regulations concerning floor flatness, structural load-bearing capacity, and other relevant site conditions, thereby ensuring stable equipment installation, operation, and maintenance.
2.5 Equipment Storage Requirements
After delivery to the factory, all equipment, components, and spare parts shall be stored in an appropriate facility that complies with applicable national standards and storage requirements.
Note: Regular lubrication and preventive maintenance shall be carried out as required. Proper maintenance is important to prevent component surface damage, corrosion, deformation, or other deterioration that may adversely affect equipment installation, commissioning, and long-term operating performance.
3. Equipment Operating Conditions
3.1 Noise Level
≤85 dB
The actual noise level may vary depending on factors such as the type and characteristics of the containers or packaging being processed, equipment operating power, and the acoustic conditions of the installation building.
3.2 Power Supply
220 VAC, 50 Hz, single-phase
Any non-standard or special power supply requirements shall be communicated and confirmed in advance.
3.3 Power Consumption
Total installed power: approximately 1.0 kW
Control voltage: 24 VDC
3.4 Compressed Air
Operating pressure: 0.5 MPa
Approximate air consumption per rejection cycle: 0.01 L
II. Equipment Introduction
1. Installation Position
The inspection system is designed to be installed on the single-lane straight conveyor section downstream of the labeling machine. This arrangement allows the system to inspect labeled PET bottles continuously as they pass through the inspection station.
2. System Operating Process
After labeling, PET bottles are conveyed continuously to the online inspection station. The machine vision system automatically captures and analyzes images of each bottle to determine whether the label is present and whether its height is within the specified tolerance range.
Bottles identified as conforming products continue along the production line, while bottles with missing labels or label-height deviations are automatically identified and rejected by the system.
The complete inspection process is performed automatically, continuously, and without physical contact with the bottles, enabling reliable online quality control at the designed production speed of 60,000 bottles per hour.
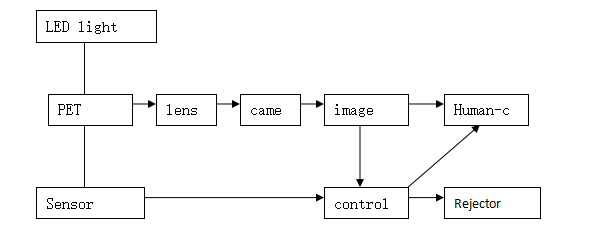
Figure: System working principle and flow chart
3. System Operation
3.1 Bottle Detection and Position Tracking
As each bottle enters the inspection station and passes the positioning sensor, the sensor detects the presence of the bottle. At the same time, the control system records the corresponding bottle identification information and encoder position value to establish accurate position tracking for subsequent image acquisition and defect rejection.
3.2 Image Acquisition and Inspection
Once the bottle reaches the predefined inspection position, the positioning sensor triggers the camera to capture an image of the bottle label. The acquired image is then transferred to the vision processing unit for analysis.
The inspection results are displayed on the HMI in real time. At the same time, the inspection data and defect information are transmitted to the control system for subsequent rejection control and process management.
3.3 Defect Rejection
When an inspection result indicates that a bottle does not meet the specified quality requirements, the control system generates a rejection signal and activates the corresponding reject mechanism.
The defective bottle is automatically removed from the production line, while qualified bottles continue through the normal conveying process.
4. Image Acquisition System
4.1 Lighting System
The inspection system utilizes a high-performance LED area light source with an expected service life of up to 50,000 hours.
The light source adopts a front-lighting configuration to provide stable and uniform illumination of the inspection area, thereby improving image contrast and inspection reliability.
Under the specified lighting conditions, the bottle opening appears in the acquired image as a continuous bright circular ring, providing a clear visual reference for image processing and measurement.
A fixed-focus manual-aperture lens is used for image acquisition. During commissioning, the focus ring is adjusted to obtain the highest possible image sharpness at the CCD sensor plane. The aperture is then fine-tuned to achieve the appropriate image brightness and contrast.
4.2 Camera
The system is equipped with an area-scan CCD analog camera with the following specifications:
Resolution: 640 × 480 pixels
Maximum frame rate: 60 fps
The camera provides sufficient image acquisition speed and resolution to support continuous online inspection at the specified production throughput.
5. Label Inspection Module Image
The label inspection module captures and processes images of each bottle as it passes through the inspection station. The acquired images are analyzed by the vision processing system to determine label presence, label position, and label orientation.
Inspection module image to be provided separately.
6. Inspection Items and Accuracy
6.1 Inspection Items
The system is designed to automatically identify the following label defects:
Missing Label
Detects bottles on which no label is present.High Label Position
Detects labels positioned above the specified height range.Low Label Position
Detects labels positioned below the specified height range.Incorrect Label Orientation
Detects labels installed in the wrong orientation, including reversed or upside-down labels.
6.2 Detection Accuracy
serial number
| Test Contents | Testing Accuracy | Rejection rate
| False rejection rate
|
1 | No label | --- | 100% | ≤0.03% |
2 | High label | Deviation ≥ 2mm | ≥99.9% | |
3 | Low label | Deviation ≥ 2mm | ≥99.9% | |
4 | Connection label (tape applied when changing labels, requires a significant color difference between the tape and label) | ≥99.9% |
7. Equipment Structure and Main Components
7.1 System Configuration
The inspection system consists of multiple vision inspection modules and a Human-Machine Interface (HMI), providing automated label inspection for high-speed production lines.
7.2 Inspection Control Unit
Each inspection module is equipped with a reliable industrial-grade control computer for image processing, inspection data analysis, and real-time communication with the central control system.
7.3 Electrical Control System
The electrical control system incorporates industrial PLCs, program memory, photoelectric sensors, proximity/inductive sensors, and other control components. Combined with dedicated control software and an HMI, these components form an integrated, highly automated, and intelligent control platform.
7.4 Reject Verification System
A dedicated reject verification module continuously monitors the rejection process to confirm that identified defective products are effectively removed from the production line, thereby preventing defective products from being passed downstream.
7.5 Electrical Control Cabinet
The power distribution and control cabinet is fitted with an industrial air-conditioning unit to maintain a suitable internal operating temperature. This helps protect electrical and electronic components and contributes to improved equipment stability and service life.
7.6 Compact Equipment Design
The inspection cabinet adopts a compact and space-efficient structural design, minimizing the equipment footprint while meeting the requirements for installation, operation, and maintenance.
7.7 HMI Monitoring and Diagnostics
Equipment operating status, inspection conditions, alarm information, and fault diagnostics are presented on the HMI through an intuitive graphical interface, allowing operators to quickly monitor system performance and identify potential faults.
8. System Advantages
8.1 High-Speed and High-Precision Inspection
The image acquisition and processing system utilizes advanced industrial-grade imported hardware, combined with dedicated image-processing algorithms. This configuration provides high inspection speed, accuracy, stability, and reliability, making the system suitable for continuous high-speed production environments.
8.2 Multi-Product Recipe Management
The system supports the configuration and storage of inspection parameters for multiple bottle types. Product specifications can be switched quickly through a simple one-touch operation, reducing changeover time and improving production flexibility.
8.3 Closed-Loop Defect Rejection Control
The integrated reject verification module provides real-time online monitoring of the rejection process. It verifies that detected defective bottles are successfully removed, creating a closed-loop inspection and rejection mechanism that improves overall quality control reliability.
8.4 Modular and Expandable Architecture
The system adopts a modular architecture with multiple communication and control interfaces, together with reserved installation space. This design provides flexibility for future functional upgrades, additional inspection modules, and system expansion.
8.5 High Reliability and Easy Maintenance
The equipment is designed for stable long-term operation, with a low incidence of failures and a straightforward maintenance structure. Routine inspection, troubleshooting, and maintenance can be performed efficiently, helping to minimize downtime and operating costs.