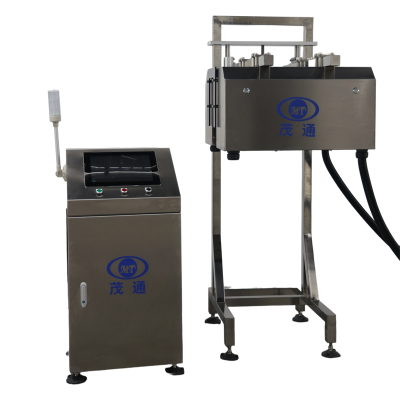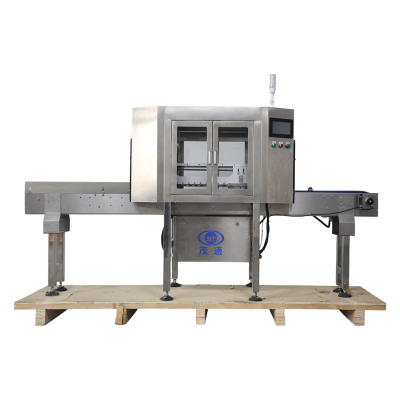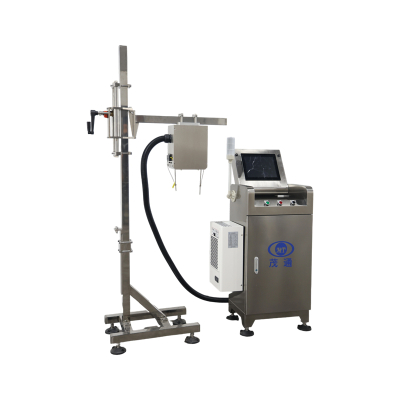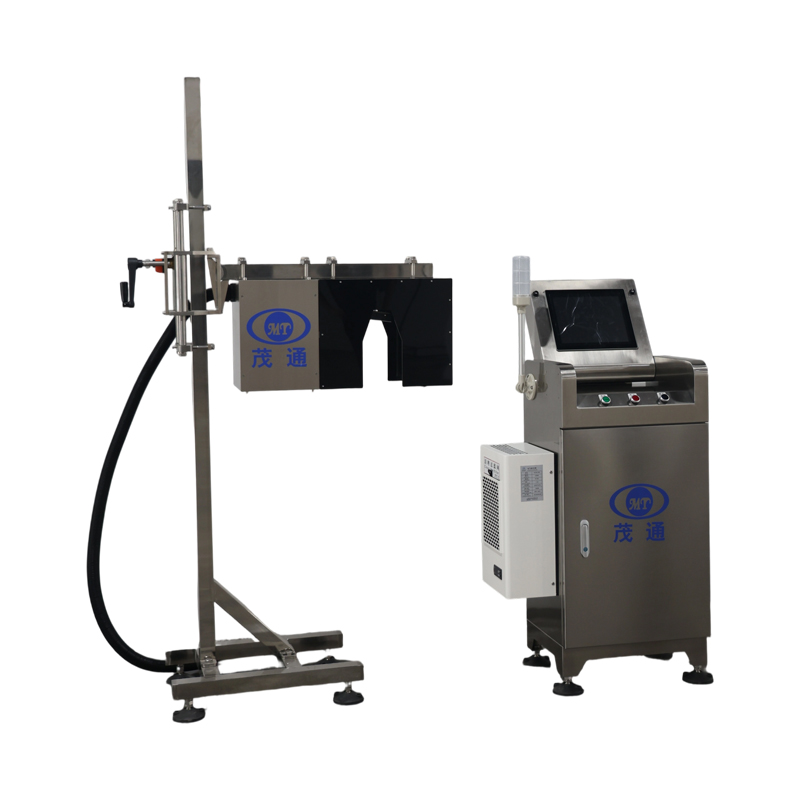

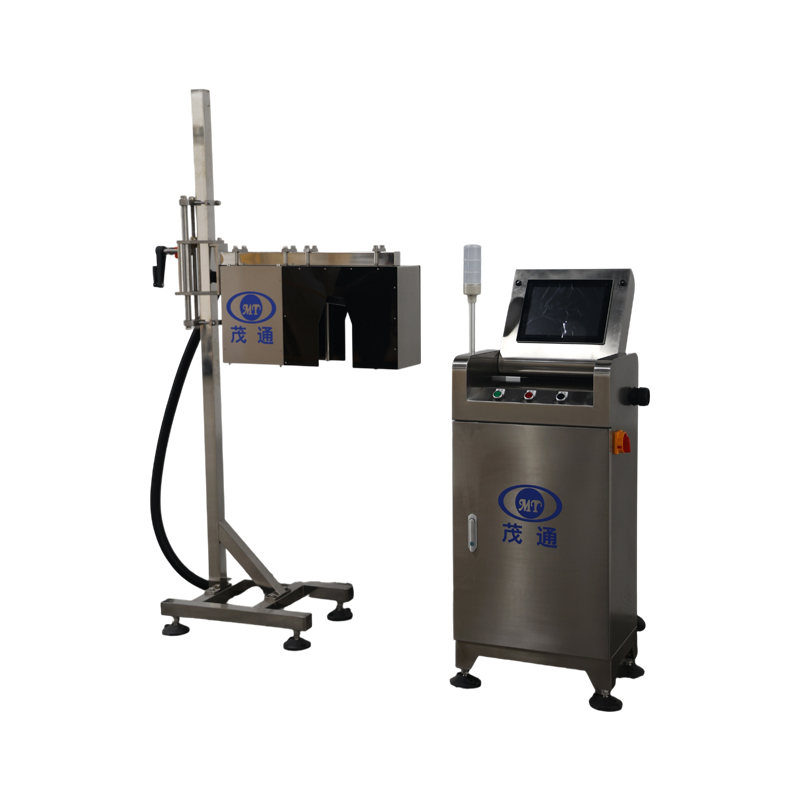
Inkjet Printing Visual Inspection Machine
1.The advanced algorithm is stable and has high detection accuracy
2.Detect different positions of code
3.The maximum speed is up to 72000 BPH
4. Equipment mechanical components
model
| Name | Components | Functional Description | Remark
|
1 | Distribution cabinet | Composed of an image processor, an interface processor, a strobe controller, and a PLC. | Provides power to the entire system, processes images, and controls the rejection of defective products. | |
2 | Detection module | LED light source, industrial CCD camera, and sensor. | Dynamically captures images of PET bottles. | |
3 | Rejection device | Main components include solenoid valves and mechanical components. | Receives signals and controls the rejection of defective products. |
5. Electrical composition of the equipment
model
| Name | Unit | Brand Notes | Quantity |
1 | Embedded imaging industrial computer (4 Ethernet ports) i5+4G+120G | Unit | Taiwan Chaoen, dust-proof, fast processing speed, and excellent stability | 1 |
2 | DAHUA high-speed gigabit digital camera | Unit | Resolution 680x480, imported from Canada, industry-leading brand | 4 |
3 | Camera I/O module | Set | Made-in-China | 4 |
4 | Lens | Piece | COMPUTAR 6MP, 12mm | 4 |
5 | Camera-50/30line cable | Piece | Made-in-China, 5m | 4 |
6 | MW.24v DC power supply 75/120W (DRP-75/120-24) | Piece | Taiwan Mean Well | 2 |
7 | PLC | Piece | Maotong independently developed | 1 |
8 | Touchscreen display | Piece | Taiwan IEI 15-inch | 1 |
9 | Light source controller | Unit | Customized in China, 4-way asynchronous triggering, screen flicker control technology, significantly extending light source life | 1 |
10 | Photo light source | Unit | Customized surface lighting, infrared, and blue | 4 |
11 | Power distribution cabinet | Piece | Made-in-China, 304 material, brushed, pickled, oxidized, and brushed finishes | 1 |
12 | Single-stage rejector Mono | Piece | Customized, air-push type, 304 material | 1 |
13 | Reject unit cylinder | Piece | Norgren high-speed cylinder, UK | 1 |
14 | Reject unit solenoid valve | Piece | MAC high-speed solenoid valve, US, 4.9ms response speed | 1 |
15 | Encoder | Piece | Made-in-China, Hode, incremental type | 1 |
16 | Low-voltage electrical components | Piece | Schneider, France | Several |
17 | Image processing system | Piece | Maotong independently developed, can develop V3.0 according to customer needs | 1 |
18 | Special equipment refrigeration unit - industrial air conditioner | Piece | Shanghai Highly Special, cooling capacity 320W | 1 |
19 | Terminal blocks | Piece | Honeywell, USA | Several |
20 | Photoelectric sensor | Piece | Leuze, Aurora PNP | 1 |
21 | Other electrical components | Piece | - | Several |
22 | Cabinet material and surface treatment | Piece | 304 material, igus® mechanical parts, brushed, pickled, oxidized, and brushed finishes. | 1 |
23 | Alarm light | - | Several | |
24 | Oil-water separator | - | Schneider tri-color tower light | Several |
25 | Relay | Piece | 1 | |
26 | Glass material | Piece | AirTac | 1 |
6. Testing cabinet structure diagram
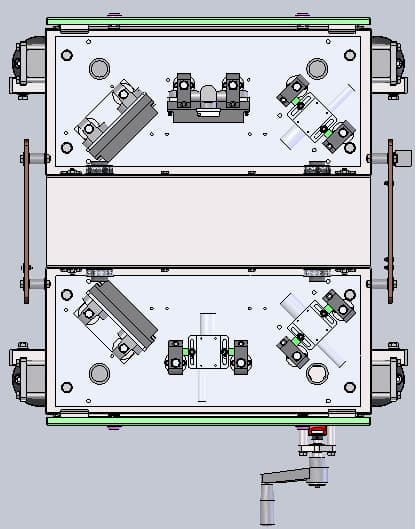
Capping liquid level detection (capping liquid level detection at stations one and three)
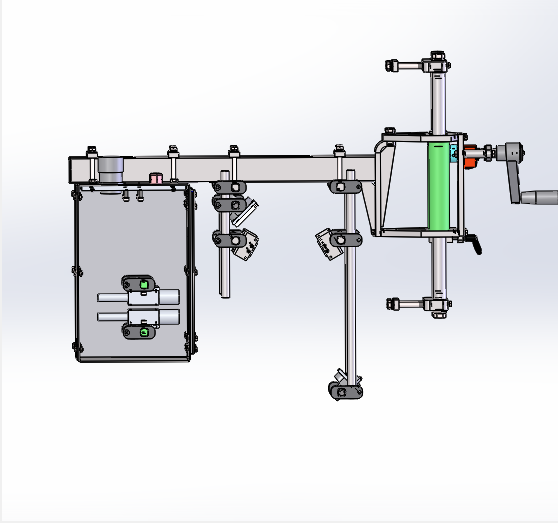
Inkjet printing inspection (station 2, single-camera inkjet printing inspection)
This inspection module utilizes three CCD cameras arranged at different viewing angles to obtain comprehensive images of the bottle, effectively reducing blind spots and improving inspection coverage. Dedicated optical lenses are used to control and filter ambient and incoming light, providing stable and clear image acquisition under varying lighting conditions. The vision system is capable of detecting a range of cap-related defects, including missing caps, tilted or improperly seated caps, cap misalignment, and damaged or broken caps.
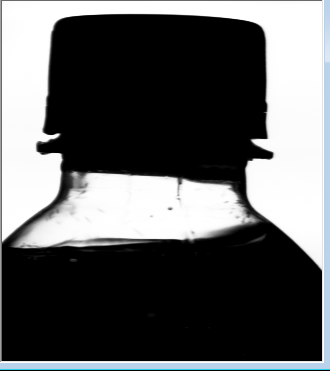
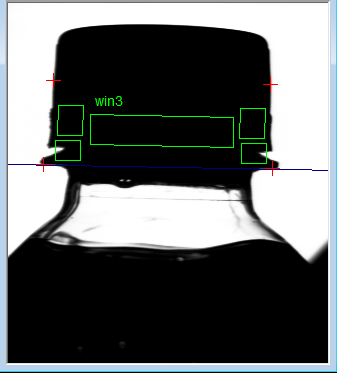
PET bottle capping images captured by CCD camera
8. Liquid Level Detection
This module employs a CCD camera to acquire front-facing images of the liquid level inside each bottle. During inspection, the bottle is positioned in a stable state to ensure that the liquid surface remains approximately horizontal, providing consistent image conditions. The vision system processes the captured image by converting the liquid-filled area to black and the empty space above the liquid surface to white. A dedicated image-processing algorithm then analyzes the resulting boundary and compares the detected liquid level with the predefined reference value to determine whether the fill level is below or above the specified limit.
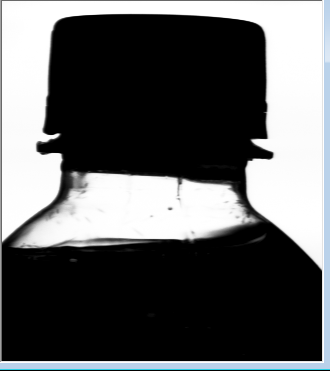
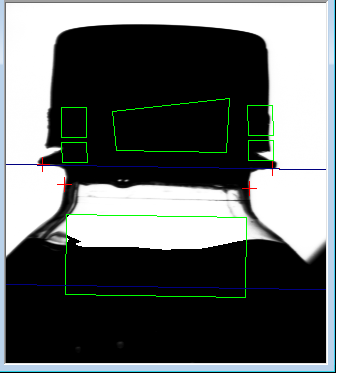
PET bottle image captured by the camera Processed liquid level detection image
9. Inkjet Printing Inspection
This module employs a CCD camera to capture front-facing images of the inkjet markings on both bottles and caps. The acquired images are digitally processed to evaluate print quality, and bottles with defective or non-compliant printing are automatically rejected. The system supports inspection for both yellow caps with black printing and black caps with white printing.
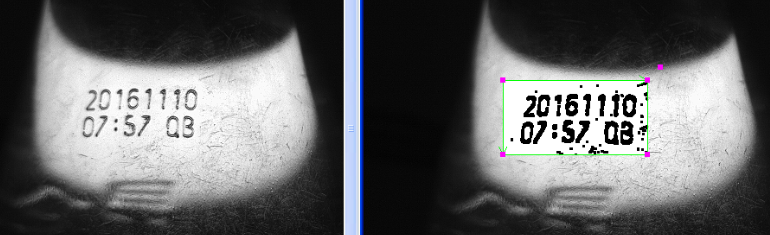
Sample image recognition processing effect
10. Detection accuracy
Inspection Items | Inspection Contents | Detection accuracy
| Rejection rate
|
| No cap | —— | ≥99.99% |
High cap | >0.8 mm | ≥99.98% | |
Crooked cap | >0.8 mm | ≥99.5% | |
Safety ring 100% disconnected | >1mm gap | ≥99.99% | |
Safety ring >70% broken | >1mm gap | ≥98.32% | |
Safety ring >50% broken | >1mm gap | ≥95.78% | |
Safety ring 100% missing | —— | ≥99.99% | |
Safety ring 70% missing | —— | ≥98.21% | |
Safety ring 50% missing | —— | ≥95.78% | |
Inspection Items | Liquid level detection (high and low) | 3mm below (or above) the standard
| ≥99.92% |
Bottle Cap Inspection | No inkjet print | ≥99.99% | |
Overall inkjet print 50% missing | ≥99.95% | ||
Overall inkjet print 30% missing | ≥99.9% | ||
Overall inkjet print 20% missing | ≥99.8% | ||
Inkjet print is blurred enough to remove the inkjet characters after processing | ≥99.99% |