
News Center
Food and Beverage Visual Inspection: How Machine Eyes Protect Production Line Safety and QualityOn high-speed food and beverage production lines, a tireless "eye" safeguards product quality and safety around the clock. This is machine vision inspection technology—it mimics human vision and combines…
2025/10/10 08:18

Visual inspection technology has penetrated every stage of dairy production, from packaging materials to finished product shipment. Its core goal is to improve the accuracy and efficiency of quality control. The following table summarizes the main application scenarios and technical highlights of…
2025/10/09 13:58

The food, beverage, and brewing industries are introducing vision inspection technology primarily to address multiple challenges, including high-quality control requirements, high-speed production pace, and cost-efficiency optimization. The following table can help you quickly understand the core…
2025/10/07 17:26
Maotong (usually referring to Jinan Maotong Inspection Equipment Co., Ltd.)'s air leakage detection equipment is widely used in the food and beverage packaging industry. It primarily uses squeeze detection technology and online automated testing to ensure packaging sealing.The following table…
2025/10/01 18:03
1. Introduction: The Importance of Can Packaging and Quality InspectionCans, as one of the most common packaging formats in the modern food and beverage industry, are widely used for packaging thousands of products, including carbonated beverages, beer, and milk powder. With the rapid development…
2025/09/25 10:57
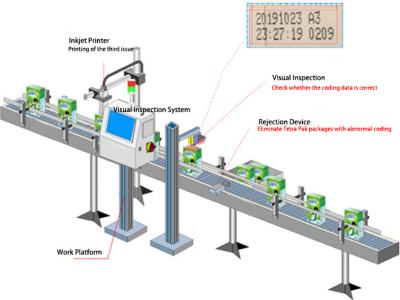
On a high-speed milk production line, Tetra Pak cartons flow through at a rate of over ten per second. A visual inspection system for coding completes inspection and determination of each product's production date within 0.2 seconds—this invisible system is a critical technological barrier to…
2025/09/24 13:24
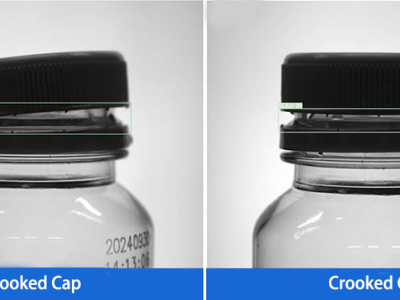
When you unscrew a bottle of mineral water, have you ever wondered what kind of "hardening" this seemingly ordinary transparent container has undergone before it reaches your hands? In the smart factory of a beverage giant, every plastic bottle undergoes a "full-body scan" by an AI vision system.…
2025/09/24 09:53

Machine vision uses machines to replace the human eye in measurement and judgment. A machine vision system uses machine vision products (i.e., image capture devices, available in CMOS and CCD) to convert captured objects into image signals. These signals are then transmitted to a dedicated image…
2025/09/22 16:17
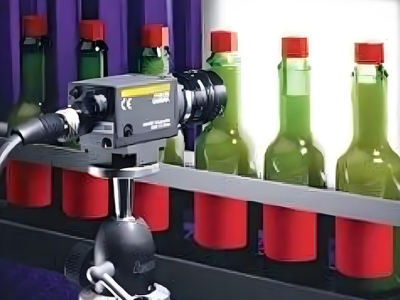
1. Core FunctionsLiquid Level Detection:Optical sensors (such as infrared and laser sensors) or vision cameras are used to detect the liquid level in bottles, preventing underfilling (impairing the consumer experience) or overfilling (causing cap leakage).Cap Detection:Checks the integrity of…
2025/09/19 14:47
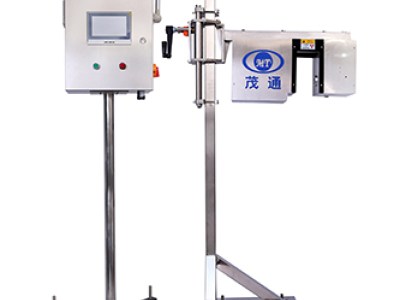
Can liquid level detection primarily utilizes photoelectric, ultrasonic, capacitance, weighing, and X-ray technologies for automated, real-time monitoring, ensuring that filling accuracy meets standards. The following are the main detection equipment and their technical features:Detection Equipment…
2025/09/19 09:40

China's machine vision industry is experiencing rapid growth by 2025, with a market size projected to exceed 21 billion yuan. The integration of 3D vision and AI will become a core growth engine, with widespread application in the automotive, semiconductor, and new energy sectors. Technological…
2025/09/19 09:01

1. Basic Situation of Online DetectionCurrently, beer production companies are increasingly emphasizing product quality, and more companies are using various automatic detection equipment on filling production lines to improve the reliability of inspections. The traditional method of checking empty…
2025/08/29 16:37
